


During a mold transfer quotation, one of the first questions should be which press will run the tool. It sounds like paperwork, but machine specifications decide whether the mold fits, runs safely, and produces the same part as before. A poor match shows up later as flash, short shots, and rework.
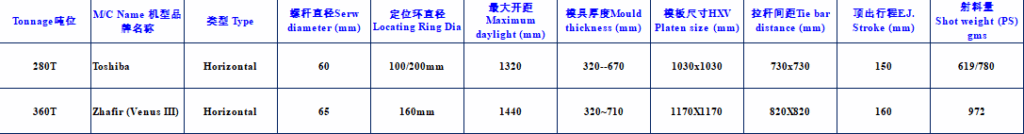
Physical Fit: Platens, Tie Bars, and Mold Height
Before design work, the mold must physically fit and install. Platen size, tie-bar spacing, mold height, and mounting details determine whether the tool can be loaded safely. A mold thicker than the available daylight cannot close, and a mold wider than the tie bars cannot enter. These fundamentals set the foundation for every later step.
Clamp Tonnage and Injection Capacity
The mold and machine must withstand the same internal forces. Tonnage, injection pressure, and clamp performance need to cover the projected area times cavity pressure, with margin. Too little clamp force produces flash and tool wear; too much can crush vents and damage the parting line. Shot size should sit comfortably inside the barrel capacity, typically between 20 and 80 percent of rated shot, so residence time stays healthy.
Ratio of Screw Diameter to Shot Weight
A small shot in a large barrel overheats and degrades; a shot near the barrel limit gives insufficient cushion. Compare the required shot weight and plasticizing rate with the recommended operating window. Thermally sensitive resins such as PC and POM tolerate narrower windows than commodity grades.
Controls, Sequences, and Auxiliary Equipment
Core pull sequences, valve gates, hot runner zones, ejector stroke, and robot interfaces must be available and programmable. A tool with three core pulls needs a controller with enough sequence steps. Dryer capacity, chiller flow, and temperature controller count belong in the same comparison, because an undersized chiller limits cycle time regardless of the press.
Validating the Match During Transfer
Moving a mold does not automatically move the process. Expect a fresh trial, sample inspection, and process window development. Compare parts from the old and new presses with dimensional reports and appearance under the same lighting. Document the approved settings so the next run starts from a known point.
Frequently Asked Questions
Can a mold run on a larger press than before?
Usually yes if tie bars and daylight allow, but residence time and clamp control change the process, so revalidation is required.
What if no press matches exactly?
Adapters and spacer plates can bridge small gaps, but check that they do not compromise safety or alignment.
How long does a transfer take?
Typical projects need several weeks for shipping, fitting, trials, and approval, depending on tool condition.
Conclusion
Injection molding machine specifications should be compared before the mold ships, not after it arrives. For related reading, see injection molding machine background, our transfer-ready mold guide, and molding process overview. Contact TCHD to match your tool.