


Injection mold quality is not a certificate or a surface finish. It is the sum of decisions made from steel selection through daily maintenance, and it shows up months later as stable output or as a stream of defects. Ten areas cover most of what determines whether a tool earns its cost.
Injection Mold Quality Starts With Steel Selection
Grade choice should follow the resin and the expected life, not the price list. Abrasive glass-filled material wears soft steel quickly; corrosive PVC or flame-retardant grades attack unpolished surfaces. P20 suits moderate volumes, H13 and S136 cover harder and more corrosive duty, and a premium grade on a short-run tool is money spent without return.
Structure Design Drives Reliability
A mature structure accounts for shrinkage, molding temperature, elastic deformation under injection pressure, cooling layout, and cycle target. Undersized support plates deflect, and the resulting flash appears as a process problem that no parameter change can fix. Ejection, slider, and lifter design belong in this stage, not in the debugging stage.
Machining Sequence and Process Planning
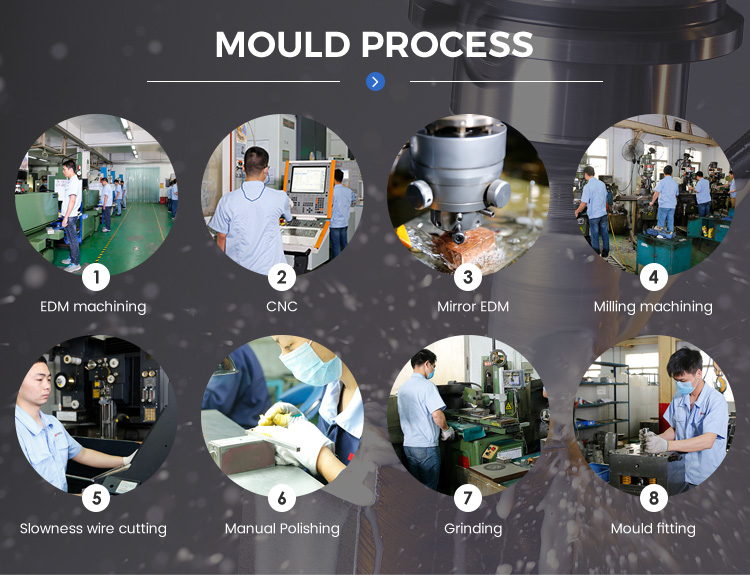
The order of roughing, stress relief, semi-finishing, heat treatment, and final finishing determines whether dimensions hold. Skipping stress relief on a large cavity insert produces movement after assembly. A clear process plan also shortens lead time, because each operation is prepared before the previous one ends.
Standard Components and Forming Inserts
Guide pins, springs, and ejector components do not shape the part, but they govern whether the tool runs smoothly for years. Brand and hardness matter more than price at this level. The inserts that form the part test the mold maker’s skill: thin walls, deep ribs, and sharp corners leave little room for error in grinding and polishing.
Polishing and Texture
Surface work is often the last operation and the easiest to rush. A polish that removes too much material changes the cavity dimension; a texture applied over a poor polish shows every scratch. Both should be planned against the drawing, with the SPI or VDI standard named.
Assembly and Fit
Assembly is precision work: every plate, screw, and dowel must sit correctly, and shut-off surfaces must close without interference. A single misplaced ejector bore can crack a core on the first cycle. Assembly records, including torque and fit checks, make later troubleshooting possible.
Runner, Cooling, and Cycle Time
Hot runner configuration is usually fixed early, so it has limited influence on quality later. Cooling is different: cycle time reductions of a second or two matter at volume, but a cooling circuit that is too aggressive distorts the part and overheats the tool. Channel diameter, density, and circuit routing should be designed with the cycle target in view.
Maintenance Decides Service Life
A mold left idle without protection rusts on forming surfaces; one run without a cleaning schedule builds scale in cooling channels. Planned maintenance covers rust prevention, vent cleaning, wear inspection on sliders, and a spare-parts list for high-wear items.
Frequently Asked Questions
Does a higher steel grade always mean better quality?
No. The grade must match resin abrasiveness, corrosivity, and expected volume, or the extra cost buys nothing.
How often should a mold be maintained?
Typically every 50,000 to 100,000 cycles for standard tools, sooner for abrasive resins or high-tonnage clamping.
What causes flash on a new mold?
Usually insufficient support or parting-surface fit rather than injection pressure, so process changes only mask it.
Conclusion
Injection mold quality is built from steel, structure, machining, assembly, cooling, and maintenance working together. For related reading, see injection moulding reference, our why cheap molds cost more, and mold partner selection guide. Contact TCHD to evaluate your tool.