
In 2014, a new project called for design and manufacture of a custom mobile phone case. The work began with customer design concepts and sample pictures, then moved through detailed reviews of the front panel, middle section, battery cover, display dimensions, and keypad before prototypes, tooling, and series production. TCHD accepts concepts, prototypes, or CAD files and handles design refinement, prototyping, and final production. Referrals account for 80% of its clients.
Front panel and surface treatment
The front panel location was fixed as shown in the customer diagram. Its surface treatment referenced the red mobile phone sample. The panel surface required painting, while the frame needed chrome plating. These finish choices affect appearance and downstream processing, so they were settled before the housing geometry was locked.

Middle section and dual SIM question
The backplate, SIM, and battery holder formed the middle section. External dimensions in L x W x H had to match the Nokia mobile phone sample, referred to as the silver middle part. Thickness remained subject to the engineers’ recommendations based on design requirements. Appearance and structure were to stay consistent with the red mobile phone sample, called the red middle part. The engineering team also asked whether dual SIM functionality was necessary, since the red phone had dual SIM slots.

Battery cover geometry
For the battery cover, the width needed to match the silver back part sample. Length was redesigned with reference to the red battery sample, and thickness again followed engineers’ recommendations. Appearance and structure were to remain consistent with the red mobile phone sample, the red battery part. The dimensions were also tailored to the customer’s display screen sample.

Keypad specifications and backlighting
The keypad dimensions and structure could follow the image labeled 5 keypad dimension. Surface finish and tactile feel were to match the image labeled 5 red keypad. All keypad markings were in Arabic, with the artwork file supplied by the customer. Backlighting changed the finish route. If the markings required backlight illumination, the surface finish would be spray painting, laser etching, and UV coating. Without backlight illumination, the finish would be silk printing and UV coating.
Prototype builds and 3D review
Two screenshots of the 3D model gave the team a shared view of the housing before cutting metal. Prototypes of the cell phone casing were then produced and tested. That work is central to agile product development: problem areas surface early, and changes can be made before commitment to production tooling. Rapid prototypes were delivered through CNC machining, 3D printing, vacuum casting, and mold-making.

Mold DFM and tool production
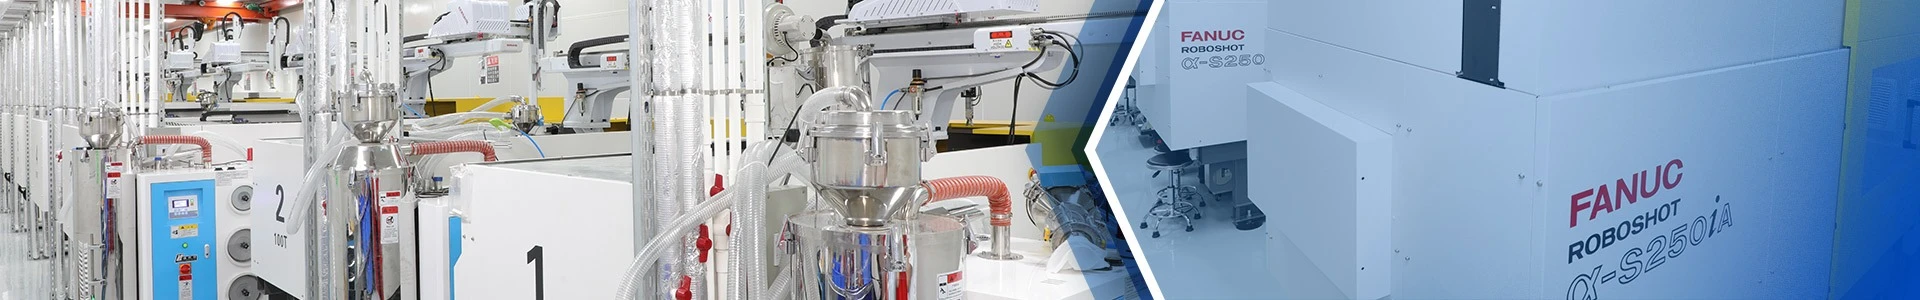
Prototype testing fed back into the design, which was optimized and finalized for manufacturability. Mold DFM and mold flow analysis supported that step. The mold production center runs imported high-precision CNC machining, spark machines, wire cutting equipment, precision grinders, and other processing equipment from Japan FUNAC, Japan Sodick, Swiss CHARMILLES, and Swiss AGIE, among others, to meet high-precision mold requirements.
Series production and inspection
Series production began after customer approval of samples. It followed the agreed quality inspection standards and the gold samples. A professional production team used a scientific and rigorous system management model to arrange the production plan and shorten production delivery time. During mold fabrication, sampling, and production, inspections used advanced testing equipment including a Sodick CMM, video measuring system, mesh tester, and color difference instrument.

For plastic injection molding work, TCHD’s capabilities can be checked against a drawing and production requirements in a technical review.