


Injection molding hidden costs rarely appear in the first quotation. They surface during parameter development, when a high-temperature resin needs a long heat soak, when a large part needs a bigger press than planned, or when a trial run consumes half a day of machine time and a barrel of material. Budgeting for those steps is the difference between a quote that holds and one that drifts.
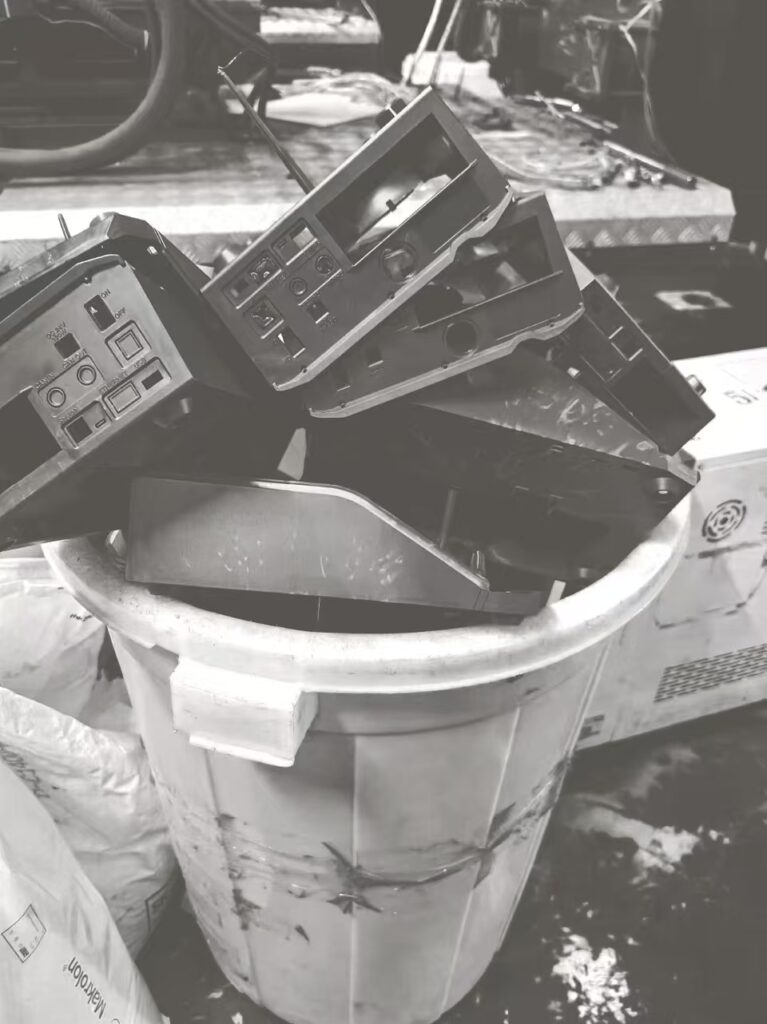
Why Specialty Resins Cost More Than Their Price
High-temperature resins, glass-filled compounds, and functional grades need higher melt temperatures, tighter control, and often a dedicated barrel or screw. They process slowly, generate more scrap during startup, and may require drying equipment and longer changeover. The purchase price is only the visible part of the cost.
The Real Cost of a Large Part
Part size drives press tonnage, mold weight, crane capacity, and energy use. Large molds take longer to heat and stabilize, so first-off parts arrive later in the shift. Handling, packaging, and storage add cost that small-part programs never see, and a machine large enough for the tool may not be available when the schedule needs it.
Injection Molding Hidden Costs in Trial Runs
Parameter development is where the uncertainty lives. A specialty material may need a slow, staged heat-up and several purges before the first acceptable part. Each adjustment burns material and machine time, and a full setup can absorb half a day. Although trial runs are planned, they are rarely scheduled with the same rigor as production.
Budgeting the Trial
A realistic plan names the machine, the material quantity, the number of parameter loops, and the approval criteria. Trials with a written checklist finish faster than trials that restart from scratch whenever a new defect appears.
Scrap and Setup Loss
Startup scrap includes purging compound, short shots, and parts made before the process is stable. On an expensive resin, a few kilograms of scrap can exceed the labor cost of the shift. Regrind helps on commodity materials but is often restricted on filled or optical grades, which turns scrap into pure loss.
Labor and Energy
Specialty programs need engineers on the floor, not only operators. Wage costs across a long setup add up quickly, and large machines draw significant power even while idling. Scheduling that keeps a big press running a single small job wastes capacity that is expensive to own.
Maintenance and Downtime
Large tools need more crane time and longer repair windows. When a heating element or a hot-runner tip fails on a big press, the downtime cost per hour is higher than on a small one, and spare-part logistics become part of the program risk.
How to Control the Budget
- Quote the tool, the trial, and the first production run as separate lines
- Confirm press availability and tonnage before committing to a schedule
- Use simulation to reduce the number of trial loops
- Agree on acceptance criteria before the trial, not after
- Track scrap by material and by cavity from the first shift
Frequently Asked Questions
Why is a trial run so expensive?
Because it consumes material, machine time, and engineering attention before a single saleable part exists.
Can hidden costs be quoted in advance?
Most can, if the resin, part size, and acceptance criteria are fixed before the quote is issued.
Is a larger press always slower to set up?
Generally yes, because of thermal mass, mold handling, and the time required to reach stable conditions.
Conclusion
Injection molding hidden costs are manageable when materials, press capacity, and trial planning are budgeted explicitly. For related reading, see injection moulding reference, our part cost optimization guide, and machine specification guide. Contact TCHD to plan your program.